Skip to content
Multi-Color SKU Development
Develop one approved womenswear style into controlled colorways, size combinations and production-ready SKUs without losing fit, fabric consistency or packing accuracy.
- MOQ starts from 200 pcs per style/color, with sizes distributed inside each confirmed color quantity.
- 6+ flexible production lines support multi-style, multi-color and multi-size production planning.
- 2 sample rooms, 7+ senior pattern makers and 20+ sample machinists support fit and sample control before bulk.
- Color, size, barcode, SKU label and carton information can be checked as part of private-label packing before shipment.
Production Capacity Built for Multi-SKU Womenswear Programs
6 Owned Factories
10+ Production Partners
100,000+ Monthly Capacity
18+ Sewing Lines
15+ QC Inspectors
12+ Merchandisers
From One Approved Style to Sellable Color SKUs
Multi-color SKU development turns one approved style into a controlled commercial structure. Every colorway must connect to the correct fabric, trims, size breakdown, labels, barcode data, packing method and bulk standard.
| Development Level | Example | Manufacturing Control Required |
| Parent Style | Dress 2408 | Pattern, construction, base size chart |
| Colorways | Black, Burgundy, Ivory, Navy, Sage | Fabric approval, shade reference, lining and trim matching |
| Size Range | XS, S, M, L, XL, XXL | Size grading, measurement points, size ratio |
| Sellable SKUs | 5 colors x 6 sizes = 30 SKUs | Color-size identification, labels, barcode mapping |
| Bulk Packing | Individual garments and cartons | SKU label, size sticker, carton mark, packing list |
| Reorder Record | Same style, new or repeated colors | Pattern, fabric, trim, packing and Golden Sample records |
Built Around the Teams Managing Fashion SKU Complexity
Merchandising Teams
Product Development Teams
Sourcing Teams
QA Teams
Common Failure Points in Multi-Color Fashion Programs
Shade Drift
Trim Color Mismatch
Fabric Behavior Changes
MOQ Fragmentation
Sample-to-Bulk Gaps
SKU Packing Errors
Womenswear Styles Developed Across Commercial Colorways

Fashion Dresses
Party Dresses
Occasion Dresses

Bodycon Styles

Corset Styles

Satin and Slip Dresses

Jumpsuits and Sets

Skirts and Fashion Tops
Build a Controlled SKU Structure Before Bulk Production
Multi-color manufacturing becomes manageable when product data is structured before materials are released. Jinfeng connects the approved style standard with color, size, label and packing information so each sellable combination has a clear production identity.

Start With the Parent Style Standard
The parent style carries the core pattern, construction and fit logic. Before multiplying colors, Jinfeng reviews the tech pack, reference sample or line sheet together with base measurements, fabric direction, lining, trims and key workmanship points. Fit-sensitive details such as bust shaping, waistline, hip allowance, strap length, armhole, neckline depth, slit position or jumpsuit rise stay attached to the style rather than being reinterpreted independently for every color.
Once the base style reaches an approved development direction, colorways are mapped against material reality. A brand may plan Black, Burgundy, Ivory, Navy and Sage, but not every shade necessarily uses an identical supplier batch or lining solution. Each color therefore needs a clear material reference and approval status before bulk release.
A well-structured parent style reduces repeated development work while preventing the opposite mistake: assuming a new color can bypass material and appearance review simply because the pattern already exists.

Convert Colorways and Sizes Into Production Identities
Every approved color is then connected to the planned size breakdown. If five colors are offered in six sizes, production is handling 30 sellable style-color-size combinations even though the sewing pattern family remains one style. Size labels, SKU labels, barcodes and packing lists need to follow the same matrix.
Jinfeng can work with size ratios inside the confirmed quantity for each color. The production team then carries style, color and size identification through cutting bundles, garment inspection and packing. For retail-ready or ecommerce-ready programs, garment-level identification can extend to hangtags, barcode stickers, color/size stickers and polybags, while carton-level control covers style, color, size, carton quantity and carton marks.
The objective is simple: the product file, the garment in hand and the carton data should describe the same SKU.
Plan Colorways Before Fabric and Sample Commitments
Core Color Plan
Fabric Availability
Development Priority
Production Readiness
Color count, quantity per color, size range, trims, packaging and target delivery window are reviewed together. Material readiness and PP approval determine when a multi-color style is suitable for production allocation.
Stock Colors and Custom-Dyed Colors Need Different Planning
Stock colors can shorten the material-development path when the right fabric and shade are available. Custom-dyed colors give stronger control over a brand-specific palette but introduce lab dips, supplier dyeing MOQ, shade approval and additional lead-time variables.
| Control Point | Stock Color Direction | Custom-Dyed Color Direction |
|---|---|---|
| Color Source | Supplier available shade | Pantone or physical reference |
| Early Approval | Fabric swatch and batch review | Lab dip or color swatch approval |
| MOQ | Based on available fabric and supplier stock | Often higher due to dyeing minimums |
| Lead-Time Effect | Usually fewer development steps | Extra color development and approval time |
| Bulk Risk | Stock continuity and batch variation | Dye lot, shade band and approval consistency |
| Trim Matching | Match lining, zipper, thread and trims to available shade | Develop or source trims around approved custom shade |
| Best Fit | Existing color direction and faster material confirmation | Distinctive brand color stories and planned volume |

Control Color Approval Before Bulk Fabric Is Released
Color approval becomes a production standard only when the physical reference, fabric surface, batch conditions and related materials are recorded clearly. Jinfeng reviews color as a material property, not a screen image.
From Pantone Reference to Bulk Color Approval
Color development can start from a Pantone number, physical color standard, approved swatch or other agreed reference. The fabric supplier may then provide a lab dip or material swatch for evaluation. Review covers hue, depth, lighting response and the visual effect created by fabric surface. Satin, velvet and other directional or reflective fabrics can look different as light changes, so approval cannot rely on a single phone photo.
When a color misses the target, the next action may be another lab dip, a closer stock shade, a new dyeing attempt or a lining adjustment. Re-dyeing is reviewed against supplier MOQ and schedule before commitment. Approval records should identify which swatch or lab dip controls the next step so production is not working from several conflicting references.
Bulk fabric is reviewed again because a correct lab dip does not remove dye-lot risk. Fabric batch, surface shine and the relationship between shell and lining remain part of the bulk color decision.
Match Lining, Print and Trim Color Around the Approved Shade
A finished garment can look wrong even when shell fabric is correct. Lining showing through pale chiffon, zipper tape visible on satin, thread contrast, metal finishes or lace tone can change the overall appearance. For printed products, print color also needs to work with the base cloth and the approved garment color story.
Jinfeng can review lining color, zipper color, thread, buttons, strap sliders, lace, decorative trims and other visible components against the approved shell. The exact list depends on the style. Structured dresses may also require cup, boning or casing decisions; matching sets require consistent color between top and bottom components.
Color approval therefore finishes only when the garment’s visible material system makes sense as a whole. Any material replacement after approval is recorded and assessed for color, cost, MOQ and lead-time impact before bulk production.
Manage a Color-Level BOM for Every Approved Colorway
A multi-color style is not controlled by changing only the shell fabric description. Every approved colorway needs a material set that tells production which components belong together.
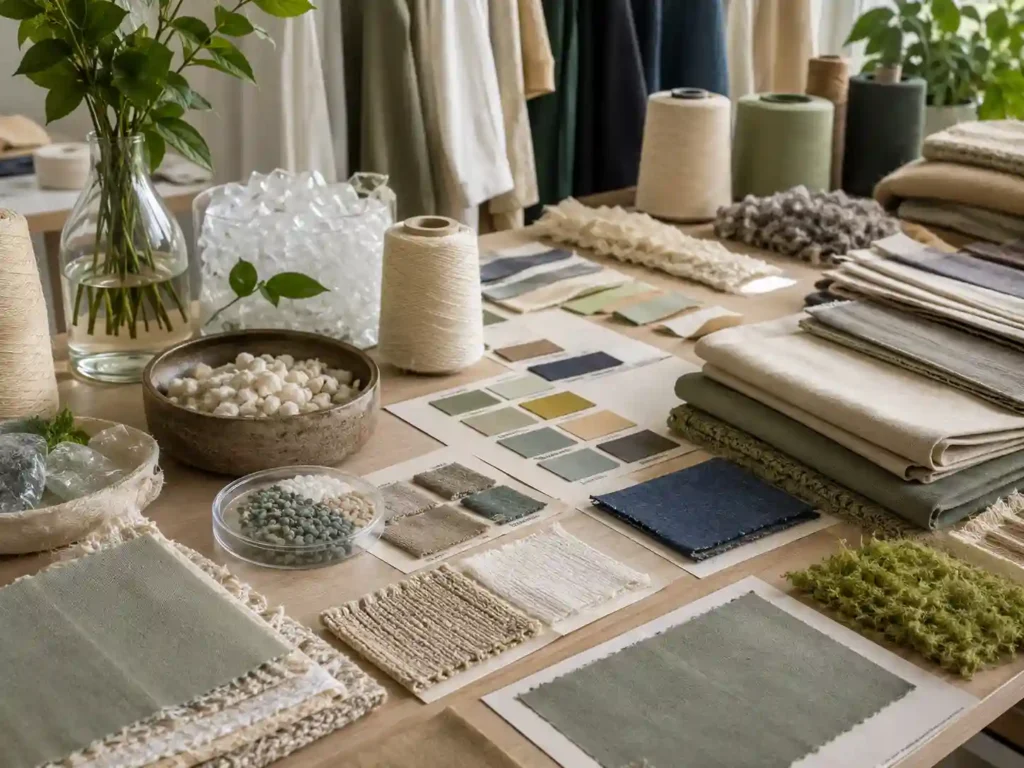
Build the Material Set Around the Garment
For a satin corset dress, a color-level BOM may include shell satin, lining, invisible zipper, sewing thread, bra cups, boning, anti-slip tape, hooks, labels, hangtags and packaging identification. A mesh party dress may add power mesh, decorative mesh, lace, sequins, rhinestones or backing materials. A matching set needs coordinated top and bottom components as well as the correct size pairing.
Jinfeng reviews material specifications, color, size, comfort, MOQ, lead time, cost and bulk availability before production. A zipper with the right tone but poor running performance is not an acceptable match. A lining that looks close on a swatch but changes the appearance of ivory chiffon needs another decision. A replacement lace may affect both color and visual pattern.
Color-level BOM control keeps the material decision connected to the approved colorway instead of relying on verbal memory during production.

Record Changes Before They Reach the Sewing Line
Material substitutions sometimes become necessary because stock changes, supplier MOQ shifts, a shade is unavailable or a sample reveals a visual problem. Jinfeng records the original item, proposed replacement and impact on color, hand feel, stretch, drape, transparency, construction, cost and timing where relevant.
Changes that affect fit or construction may require pattern review or another sample. Changes limited to a visible trim may still require approval before bulk purchase. Once the final BOM and trim direction are confirmed, the same references move into PP approval, production handover, QC and packing preparation.
A clean BOM path reduces a common multi-color failure: one color being produced with an unapproved lining, zipper, thread or trim because several versions were discussed during development.
Sampling and Revision Control Across Multiple Colorways
Sample development establishes fit, construction and material standards before the complexity of multiple colors enters bulk production. Jinfeng separates sample stages and records revisions instead of treating the first sample as the final manufacturing standard.

Establish Fit First, Then Control Color-Specific Changes
A normal dress sample commonly requires around 10-15 days. Complex corset, sequin, lace or mesh styles commonly require around 15-25 days, or longer when material, trim or structural development needs more work. Sample timing is confirmed by project rather than promised as one fixed number for every garment.
Development may include first sample, fit sample, revised sample, photo-ready sample, PP sample and Golden Sample depending on the program. The first sample is used to expose fit, fabric and construction issues; it is not automatically the bulk standard. Fit review can cover bust, waist, hip, dress length, strap length, armhole, neckline depth, slit height and jumpsuit rise where relevant.
Once fit direction is stable, additional colorways can be evaluated for fabric behavior, transparency, lining, trim matching and surface appearance. A pale color may need a different lining decision, while a custom-dyed color may require lab dip approval before a full sample is worthwhile.

Convert Every Approved Revision Into Production Files
Revision control matters more as color count increases. Jinfeng records the problem, cause, change, cost impact, timing impact and whether a revised sample is needed. Bulk-relevant changes are transferred into updated pattern, size chart, BOM, fabric record, trim record, sewing instruction, QC checklist and packing instruction.
A fabric change is not treated as a cosmetic swap. Different weight, stretch, recovery, drape, transparency or shrinkage can affect fit and construction. A trim change may alter comfort or visual balance. Color corrections can require another lab dip or a new bulk-color approval.
PP development begins only after fit, fabric, color, trims, construction, packaging, MOQ and production-related conditions are clear enough to lock. The result is a traceable path from development comments to a production standard the bulk team can actually follow.
Keep Fit and Size Logic Stable Across Color SKUs
Base Size Control
Size Grading
Size Ratio Planning
Fabric-Fit Review
MOQ Planning for Multi-Color Womenswear Collections
One Style, One Color
One Style, Two Colors
One Style, Two Half-Colors
Custom Color or Special Material
More Colors Change Cost Beyond the Fabric Price
Fabric Commitment
Trim Matching
Cutting Separation
QC Workload
Packing Complexity
Commercial Optimization
Cost can often be controlled without weakening brand-level appearance by consolidating weak colors, using suitable stock-fabric directions, optimizing size ratios, simplifying non-critical construction or planning split shipment by launch priority.
Lock PP Standards Before Multi-Color Bulk Production
Bulk consistency depends on a clean transfer from approved development files into production. PP lock turns the final decisions on fit, materials, color, construction and packing into the working standard for the production team.

Transfer the Approved Style Into a Bulk Control Pack
After development approval, Jinfeng transfers final pattern, size chart, fabric reference, color approval, trim card or BOM direction, sewing instruction, label placement, packing instruction and QC checklist into the bulk production handover. The objective is to remove gaps between the people who developed the sample and the people responsible for cutting, sewing, inspection and packing.
For a multi-color style, the handover also identifies which materials belong to each colorway. Shell, lining, zipper, thread, visible trims and packaging identification should not be left open once bulk purchasing and cutting begin. Size ratio and color quantity are confirmed before production planning so cutting and packing data follow the same order structure.
Production schedule is confirmed after PP approval according to quantity, color count, material readiness, construction, packaging requirements and available production allocation. A single fixed bulk lead-time promise is not used for every program.
Keep PP-Locked Items From Drifting During Production
PP lock covers fabric, color, trims, measurement, construction, labels, hangtags, polybags, carton marks and packing method as applicable. Late changes can affect material availability, price, schedule and bulk consistency, so they are handled as formal change requests rather than casual messages.
If a brand changes one color after PP, Jinfeng reviews whether the new shade affects fabric sourcing, lining, trim color, MOQ, sample approval or production timing. If a packaging file changes, barcode or carton information may also need updating. If fabric stretch changes, pattern and measurement standards may need another review.
The same discipline protects a multi-color program from gradual version drift: one color using an old trim file, another using a revised size chart, and a third carrying a different packing instruction.
Flexible Production Supports Multi-Style and Multi-Color Programs
Flexible Line Planning
Product-Based Allocation
Material-Ready Scheduling
Unified QC Direction
Multi-Color QC From Fabric Receipt to Final Packing
A color program is only stable when quality checks follow the SKU structure through every production stage. Jinfeng’s QC path covers materials, cutting, sewing, measurements, finished garments and packing rather than depending only on a final inspection.
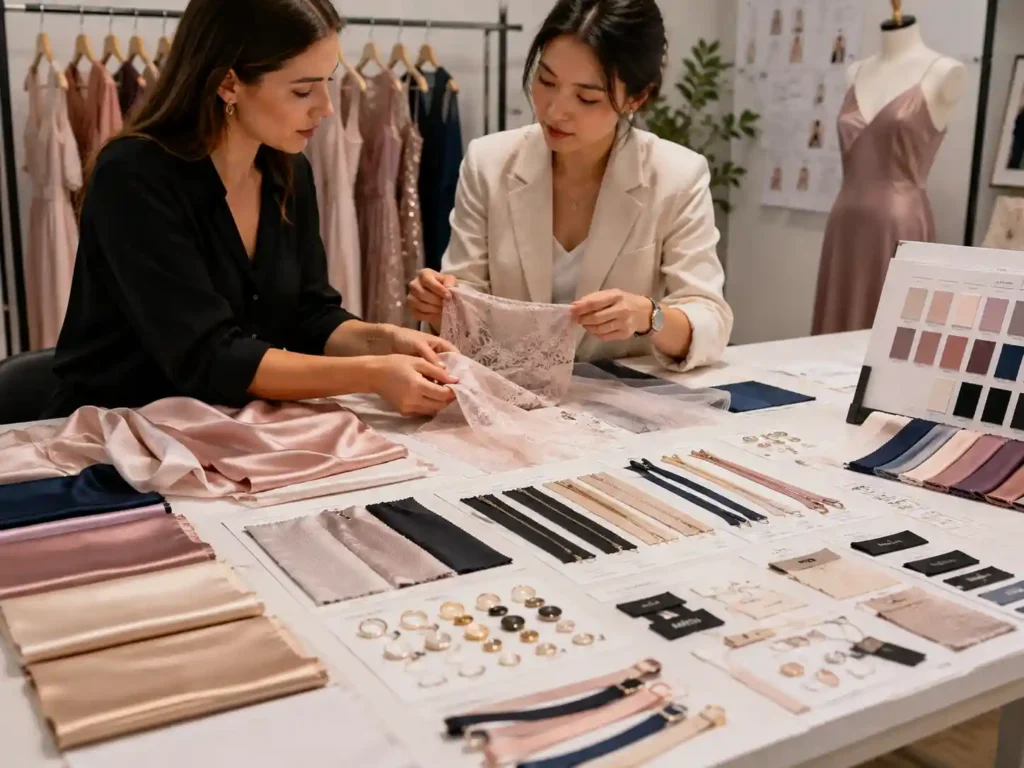
Incoming Fabric and Color Control
Incoming review checks fabric color, batch, width, weight, hand feel and visible defects according to the approved material direction. Risk points change by fabric: satin can show shade variation and snagging; mesh can show holes, unstable stretch or transparency changes; lace needs pattern and edge review; sequin fabric can show shedding or surface damage.
Color approval records are used as references for bulk fabric review. Dye lot, surface shine and lighting can change perceived color, especially on satin and velvet. Shell and lining are reviewed together when transparency or color cast affects the finished garment. When a material fails the approved direction, the issue is handled before cutting wherever possible rather than trying to hide it later in sewing.
Cutting then follows the correct pattern, fabric direction, stretch direction, print or lace placement, quantity and size bundles. Color groups remain separated so bundle identification does not create downstream SKU mixing.

Sewing, Measurement and Finished Garment Control
In-line sewing checks focus on style-specific construction: seam quality, symmetry, zipper flatness, straps, ruching, lining, slit, lace application, corset structure or other approved details. Multi-color programs also verify that the correct trims and lining are being used for the correct shell color.
Measurement control compares bulk garments with the approved size chart and agreed tolerance points. Bust, waist, hip, length, strap, armhole, neckline, slit and jumpsuit rise can be checked according to product type. Finished garment inspection then reviews appearance, pressing, stains, holes, loose threads, zipper or button function and the overall visual consistency expected from the approved sample.
Different colorways can reveal different defects. Pale colors expose lining and stains more easily; dark satin can show pressing marks or shade changes; sequins and lace create separate handling risks. QC therefore follows the material and garment, not a generic checklist alone.

Packing QC Protects the Sellable SKU
Final packing checks whether the garment inside the bag matches its size label, color identification, hangtag, barcode, SKU label and packing instruction.
Carton-level control covers quantity, style, color, size, carton mark and packing-list consistency before shipment.
For ecommerce-ready or retail-ready orders, a garment can be perfectly sewn and still create operational loss if the barcode belongs to another color or the carton breakdown is wrong.
Packing QC is therefore part of product quality, not an administrative step after production.
Keep Every SKU Accurate Through Private-Label Packing
Multi-color programs reach the warehouse as individual commercial units. Private-label packing connects the approved garment to the brand’s size, color, SKU, barcode and carton system.

Garment-Level Identification
Jinfeng supports private-label elements such as woven labels, size labels, care labels, hangtags, barcode stickers, SKU labels, color or size stickers and polybags according to the approved program. Each garment is checked so the physical product and its identification match before it enters the carton.
A five-color, six-size style may create 30 sellable combinations. Packing teams therefore work from structured style-color-size information rather than visual guessing. Pale pink and blush, navy and black, or two close green shades can be difficult to distinguish under warehouse lighting, so readable SKU and color identification are essential.
Custom labels, printed polybags, hangtags or other packaging items may carry separate supplier MOQ. Artwork, barcode lists and placement instructions should be reviewed early enough to avoid packaging becoming the last unresolved part of production.
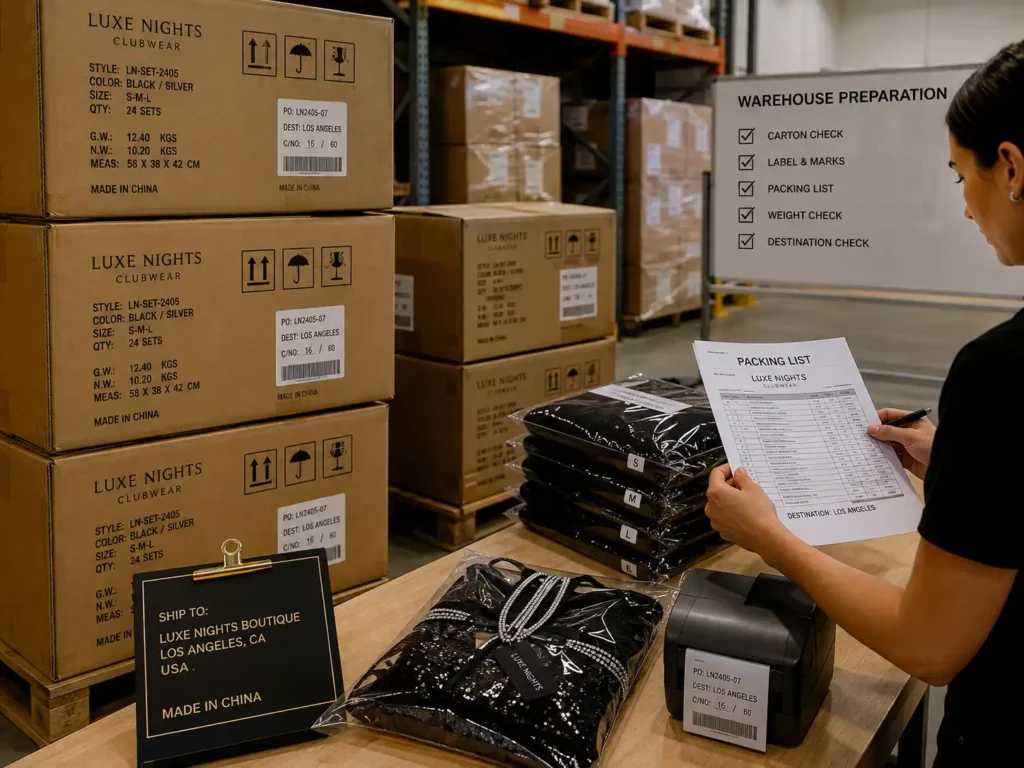
Carton Data and Warehouse Readiness
Carton-level information can include style, color, size, pieces per carton, carton quantity, carton number, carton mark, gross weight, net weight and carton measurement where required. Packing lists use the same breakdown so the brand, forwarder and warehouse can identify what each carton contains.
Multi-batch delivery can also be organized around launch priority, color group, size ratio, region, warehouse destination or split air/sea shipment when a project requires it. Every split needs clear carton data and documents; dividing shipment without dividing SKU information creates more risk, not more flexibility.
The goal is a clean handoff from manufacturing to receiving: the garment, polybag, barcode, carton and packing list all describe the same unit.
Extend Proven Styles Into New Colors and Reorders
A successful style often grows through repeat production, new colors or seasonal extensions. Jinfeng keeps development and production records so approved work can support the next program without treating every reorder as a completely new garment.

Reuse the Right Records, Not Old Assumptions
For confirmed styles, Jinfeng can retain pattern records, size grading, fabric references, trim records, sewing instructions, packing records, QC notes and Golden Sample information. These records help repeat orders start from an established standard and support same-style new-color development or same-pattern fabric extensions.
Reorder preparation still includes a fresh check of fabric availability, batch, color, trim availability, quantity, PP or color-sample need, packing and delivery plan. An old fabric name does not guarantee the same hand feel or dye lot is still available. A new burgundy may need color approval even when the black version has been produced successfully for several seasons.

Use Sales Results to Expand the Color Program in Stages
Brands do not need to launch every possible shade at once. A stronger production strategy can begin with an approved core color group, then add new colors after the style proves commercially useful. Multi-color MOQ still applies to each added color, and new fabric or custom dyeing requirements are reviewed before production.
For replenishment, priority colors and sizes can be identified early, then production and packing are organized around the confirmed reorder structure. When a new color uses the same pattern but a different fabric weight, stretch, lining or trim set, development review protects the original fit and appearance rather than assuming the old files can be copied unchanged.
A Representative Multi-Color Program at Current Brand Scale
Current cooperation programs commonly involve 10-30 styles per brand order with total quantities in the 20,000-80,000 piece range. The example below shows how a realistic multi-color order can be structured and controlled without exposing brand identity or confidential project files.

Example Program Structure: 18 Styles, 54,000 Pieces
A representative order can contain 18 fashion womenswear styles, five commercial colorways per style and six sizes per color. At an average 600 pieces per style/color, the order reaches 54,000 garments. The style-color-size matrix contains 540 sellable SKU combinations before any warehouse-specific carton or regional allocation is added.
Such a program is not managed as one 54,000-piece PO. Development begins by grouping styles according to fabric, construction and risk. Satin, mesh, stretch, lace and structured styles may follow different sampling and material paths. Color plans are checked against stock availability or custom-dye requirements, then quantity per color and size ratio are confirmed. Fit is controlled at style level, while color-specific fabric, lining and trims are approved before bulk release.
Sampling capacity, merchandising follow-up and production allocation matter because 18 styles may not reach PP status on the same day. Styles move forward according to material readiness, revision status and launch priority rather than waiting for every SKU to become ready at once.

Execution Focus: Keep 540 SKUs From Becoming 540 Problems
Once PP standards are locked, production files identify final pattern, size chart, BOM, color references, trims, sewing instructions, labels, packing and QC checkpoints. Cutting bundles remain separated by style, color and size. In-line checks verify construction and correct trim usage. Measurement review protects size consistency across color groups.
Packing creates another control layer. Every garment needs the correct size label, SKU or barcode identification and polybag instruction; cartons need accurate color-size breakdown and marks. A packing list then ties the shipment data back to the order structure.
A program at 20,000-80,000 pieces succeeds through disciplined information transfer rather than one dramatic factory claim. The same logic also supports later replenishment: confirmed patterns, fabric references, trim records, packing standards and Golden Sample information create a cleaner starting point when a proven style returns in another color.
Multi-Color SKU Frequently Asked Questions
Send Your Multi-Color SKU Development Plan
A useful project review starts with enough information to understand the style, color structure and intended bulk program.
Send a tech pack, reference image, line sheet or original-sample photos together with the planned color list and quantity per style/color. Include fabric direction, size range, label or barcode requirements, packaging instructions and target delivery window when available. Jinfeng will review development feasibility, material direction, MOQ, sample route, production risks and the information needed before a more accurate quotation can be prepared.
Please include:
- Company and product category
- Tech pack, reference image or line sheet
- Number of styles
- Planned color list
- Quantity per style/color
- Size range and size ratio
- Fabric or material direction
- Custom-dyed color requirements
- Label, barcode and SKU files
- Packing or warehouse instructions
- Target delivery window
- Any NDA or file-protection requirement